Executive Summary
This engineering guide solves wear and structural degradation issues in commercializing designer homeware collaborations.
Spatial Philosophy & Architectural Narrative
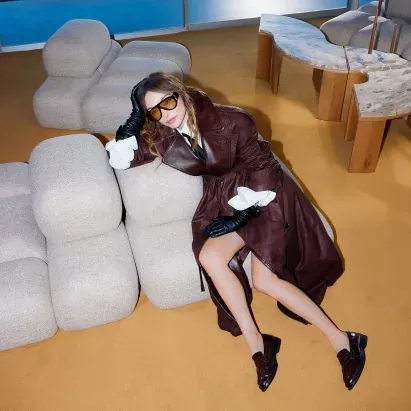
In contemporary commercial and hospitality spaces, designer-collaborated FF&E elements are not mere visual highlights but critical media for brand narrative. The spatial layout of these pieces must adhere to a rigorous structural hierarchy. From lobby transition zones to executive lounges and private guestrooms, furniture volume and scale must synchronize with architectural circulation and light paths. Regarding lighting design, the distinct material characteristics—such as the micro-crystalline texture of natural stone and the diffuse reflectance of metallic trims—require narrow-angle warm spotlighting to emphasize geometric silhouettes and raw textures, avoiding the flattening effect of ambient lighting. Spatial flow dictates that furniture layouts act as directional cues, utilizing height variations in sofas and lounge chairs to define social boundaries without physical partitions. This spatial philosophy elevates product design into functional spatial vessels, ensuring high-traffic hospitality spaces communicate a refined, highly recognizable brand identity while maintaining operational flow. The integration of lighting, spatial volume, and material texture forms a cohesive interior environment.
Luxury FF&E Material Engineering & Joinery Breakdown
Translating designer furniture into high-traffic commercial environments requires systematic engineering re-development. For structural substrates, all millwork and loose furniture frames must utilize CNS 1349 F1-grade low-formaldehyde moisture-resistant plywood, with moisture content maintained strictly between 8% and 12% to prevent delamination and warping. For joinery, standard adhesive bonding is insufficient for commercial tensile and shear stresses. Intersections must deploy a hybrid method combining double wooden dowels and high-strength eccentric cam connectors. Hardware must be certified under DIN EN 15570, featuring soft-closing hinges and damping drawer runners tested to 100,000 open-close cycles, ensuring the frame sustains a 150 kg alternating load without structural deformation.
Metallic trim details represent the core of high-end joinery. All metal components must utilize SUS304 stainless steel treated with PVD (Physical Vapor Deposition) titanium coating. The coating thickness must be no less than 1.5 microns with a hardness of HV800+ to resist scratches and oxidation from daily cleaning. Natural stone components, such as table tops, must be 20 mm thick and backed with high-strength epoxy fiberglass mesh. A 3 mm anti-vibration elastic cushion pad must be installed between the stone and the wood substrate to distribute localized impact loads and prevent natural fissure propagation.
The physical performance of soft-furnishing fabrics dictates operational lifespan. All upholstery fabrics must survive over 40,000 Martindale rubs without pilling or yarn breakage, with a tear strength exceeding 350 N. To comply with fire safety codes, the combined system of fabric and high-density fire-retardant foam (density >= 45 kg/m³) must pass the BS 7176 Medium Hazard standard. Specifically under the Crib 5 test (wood crib heat release rate of 5.2 kW), the assembly must self-extinguish within 10 minutes without releasing flaming droplets, supported by accredited third-party test reports to ensure life safety and physical durability in commercial settings.
Hospitality Operations, Wear Analysis & TCO Model
In luxury hotel and commercial real estate asset management, the Total Cost of Ownership (TCO) of FF&E directly affects Net Operating Income (NOI). High-frequency impact and fabric wear typically peak between years 3 and 5 of operations, often forcing complete furniture replacement or expensive onsite touch-ups. To mitigate recurring CapEx, asset managers should mandate modular, detachable maintenance structures and replaceable upholstery systems.
Taking guestroom sofas as an example, high-contact zones like armrests and seat cushions are designed as separate, detachable units. In the event of localized cigarette burns or cosmetic staining, staff can swap the specific upholstered module onsite within 15 minutes, reducing maintenance costs to just 8% of full replacement expenses. Financial modeling shows that upgrading to soil-resistant coatings (such as Teflon or Crypton treatment) and increasing Martindale wear to 50,000 rubs increases initial procurement costs by 12% but extends the localized refurbishment cycle from 3 years to 6 years.
Discounted cash flow (DCF) simulations demonstrate that over a 10-year operational cycle, this engineering strategy reduces cumulative maintenance and replacement costs per room by 35%, optimizing the asset balance sheet. Furthermore, a scheduled preventive maintenance program—comprising semi-annual hardware lubrication and stone crystal-surface polishing—retains a residual furniture value of over 20% of the initial cost by year 8, providing financial flexibility for property repositioning.
Sunder Engineering Grounding & Subtropical Climate Defense
For the high-temperature, high-humidity subtropical island climate of the Asia-Pacific region, where relative humidity routinely hovers between 75% and 85%, factory-level fabrication and finishing must deploy precise physical defense measures. First, timber substrates must undergo moisture content verification using high-frequency pinless moisture meters at three critical stages: raw material receipt, machining, and pre-shipping. Moisture levels must be stabilized at 9% (plus or minus 1%).
To prevent airborne moisture penetration, all panel cutouts, millings, and dowel holes must receive double-sided sealer coatings prior to final assembly. Edge banding must bypass conventional EVA hot-melt adhesives in favor of PUR (polyurethane) reactive hot-melt adhesive, which offers three times the water and heat resistance of EVA, preventing edge delamination caused by hygrothermal expansion.
Structural joinery must incorporate expansion gaps of 1.2 mm to 1.8 mm at the interfaces between solid timber and composite panels, filled with high-elasticity anti-mildew polyurethane sealant to absorb seasonal wood movement. Factory fabrication should utilize a highly modular prefabrication strategy, finishing 90% of structural joinery and finishing work within a temperature-controlled, dust-free plant (22 degrees Celsius, 55% RH). This minimizes onsite installation time by 40% and shields finishes from construction-site moisture and dust, ensuring paint film adhesion meets the ASTM D3359 5B standard.
B2B Material & Inspection Specification Table
To ensure the structural integrity and aesthetic fidelity of designer FF&E, the following multi-line markdown table outlines the essential material specifications and inspection standards required for B2B procurement and site handover.
| Component | Specification | Inspection Standard | Tolerance & Criteria |
|---|---|---|---|
| Wood Substrate | F1-grade moisture-resistant plywood, double-sealed | CNS 1349 / EN 312 | Formaldehyde ≤ 0.3 mg/L, moisture content 8%-12% |
| Hardware Hinges | SUS304 heavy-duty soft-closing dampening hinges | DIN EN 15570 Level 3 | Drop ≤ 0.5 mm after 100,000 cycles |
| Metal Finishing | SUS304 stainless steel with PVD titanium coating | ASTM B117 / ISO 9227 | Salt spray test 96h without corrosion, thickness ≥ 1.5 μm |
| Fabric Upholstery | Fire-retardant fabric with high-density foam | BS 7176 Medium Hazard | Martindale rubs ≥ 40,000, Crib 5 compliance |
| Natural Stone | 20mm marble with high-strength epoxy fiberglass mesh backing | ASTM C97 / ASTM C170 | Flatness tolerance ≤ 0.3 mm, compressive strength ≥ 80 MPa |
Quality assurance engineers must perform random onsite verifications using digital calipers and gloss meters. Particular attention should be paid to joint alignment and PVD color consistency to guarantee that the delivered FF&E aligns with the engineering standards expected of commercial assets.